Multitasking turn-mill or a lathe with live tools: which do your parts need?
A part needs a multitasking turn-mill when it has holes or faces at several angles, which take a milling head that tilts on a B axis, or more tools than a turret holds, which take a tool magazine. Otherwise, a lathe with live tools, a Y axis and a sub-spindle turns, drills, taps and mills it, off center and on both ends, in one setup.
Published Nov 10, 2026
What are the steps from a lathe to a turn-mill?
Each step does work that would otherwise take a second setup or a second machine. Your parts decide how far up you need to go.
| Step | What it does | On these machines |
|---|---|---|
| Live tools and a C axis | Driven drills, taps and end mills in the turret; the C axis indexes the part | CUTEX-180 except STD; Hi-TECH 350, Ultima B620 SLY, C1, C2 |
| Y axis | Moves the tool off the centerline | CUTEX-180 YMC and YSMC; Hi-TECH 350, Ultima B620 SLY, C1, C2, i2 |
| Sub-spindle | Takes the part over to machine the back end | CUTEX-180 SMC and YSMC; Hi-TECH 350, C1 and C2 YSMC; Ultima B620 SLY, i2 |
| Tool magazine | Holds more tools and changes them automatically | C1 and C2, 12 tools; i2, 40 (80 optional) |
| B-axis milling head | Tilts a milling spindle to cut at an angle | i2, ±120° |
What do live tools and a Y axis add?
Live tools are driven drills, taps and end mills in the turret. With the C axis turning the part to each position, they drill and tap the end face and the diameter and mill slots, so the part skips the mill. On the Hi-TECH 350 they run to 5,000 rpm and take drills to Ø0.79 in (Ø20 mm) and taps to M16.
A Y axis moves the tool off the centerline. Eurotech lists what the Ultima B620's Y axis does: flat milling, irregular slots, keyways, thread milling, and drilling and milling hole patterns (brochure p. 8). Travel sets how far off center the tool reaches: ±2.17 in (±55 mm) on a Y-axis CUTEX-180, ±2.36 in (±60 mm) on the Hi-TECH 350, 3.54 in of stroke on the Ultima B620.
Hwacheon offers these steps as builds. The CUTEX-180 comes as STD for turning only, MC with a live-tool turret and a C axis, YMC with a Y axis, and SMC or YSMC with a sub-spindle on the long bed. The Hi-TECH 350 has the Y axis and the live-tool turret with its C axis as standard, and its YSMC adds a sub-spindle. The Ultima B620 we list is the SLY, with all three. On the CUTEX-180 and Hi-TECH 350, the axial and radial live holders themselves are options (CUTEX-180 catalog p. 8, Hi-TECH 350 catalog p. 13).
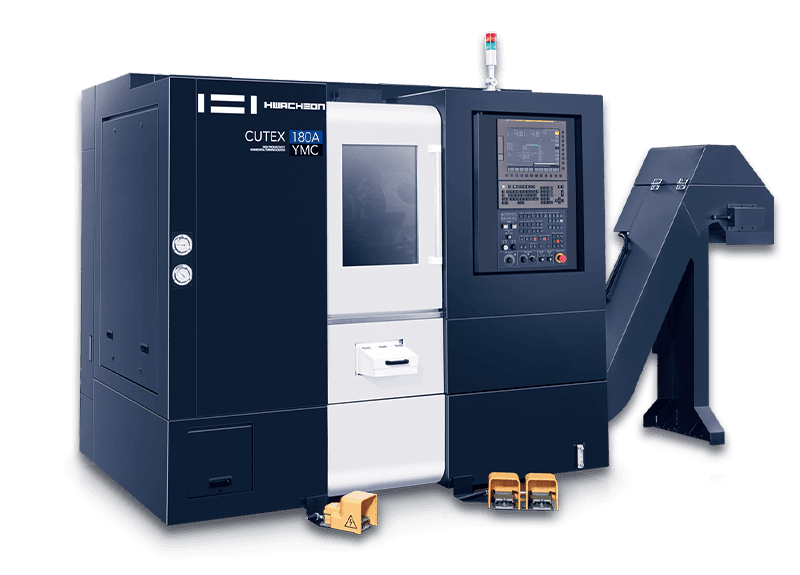
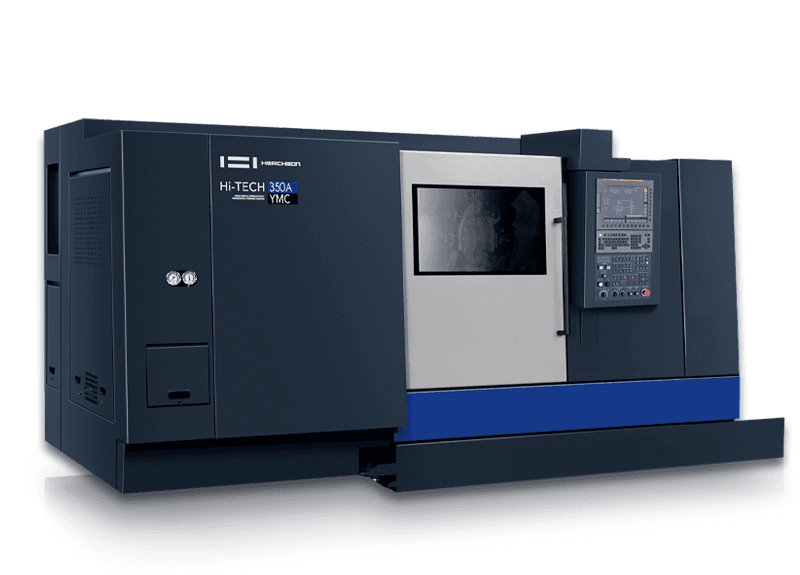
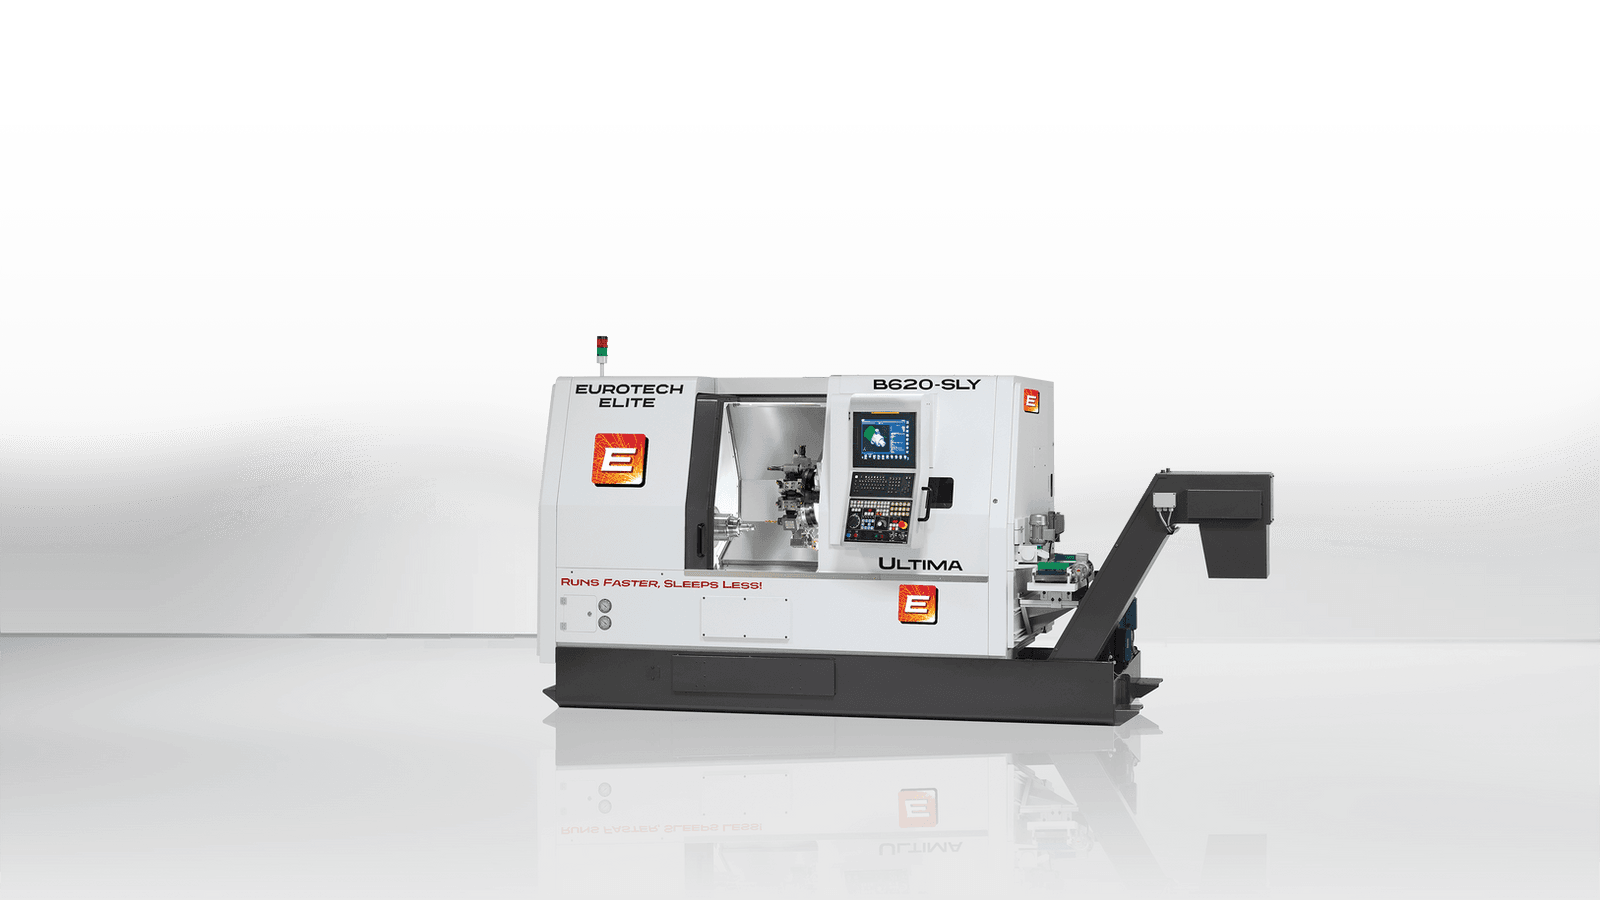
To see which are on the floor today, check new machines in stock.
What about the back end of the part?
That is the sub-spindle's job. Hwacheon's Hi-TECH 350 and T2 catalogs draw it in three steps: the main spindle machines the first end, the sub-spindle picks the part up, and the second end is machined there (Hi-TECH 350 p. 8, T2 p. 6). Without one, the part comes out, gets turned around and clamped again, or goes to a second machine.
With its own C axis, a sub-spindle gets live-tool work too. The Ultima B620 SLY's 5,000 rpm sub-spindle has one (brochure p. 3, 9, 19).
Check the sub-spindle on its own terms: it can be smaller than the main spindle. On the C2 YSMC the main spindle takes an 8 in chuck and Ø2.56 in (Ø65 mm) bar, the sub-spindle a 6 in chuck and Ø1.14 in (Ø29 mm) bar (C1 / C2 catalog p. 18).
What if the part needs more tools than the turret holds?
Count every tool the part takes, both ends. A turret holds a fixed number: 12 stations on the CUTEX-180 and Hi-TECH 350, 15 on the Ultima B620. Some take more than one tool per station: the CUTEX-180's live-tool builds index to 24 positions for double holders (catalog p. 6, 8), and Eurotech says up to 30 tools can be used together on the Ultima (brochure p. 6).
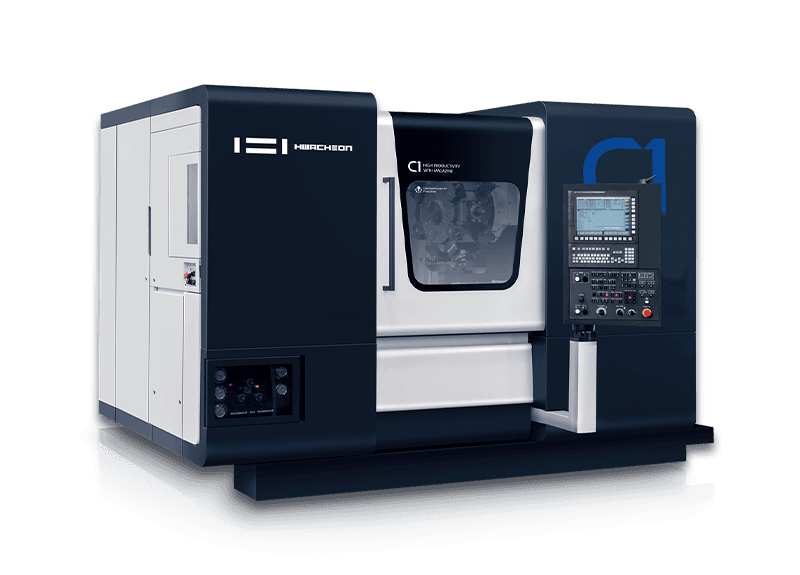
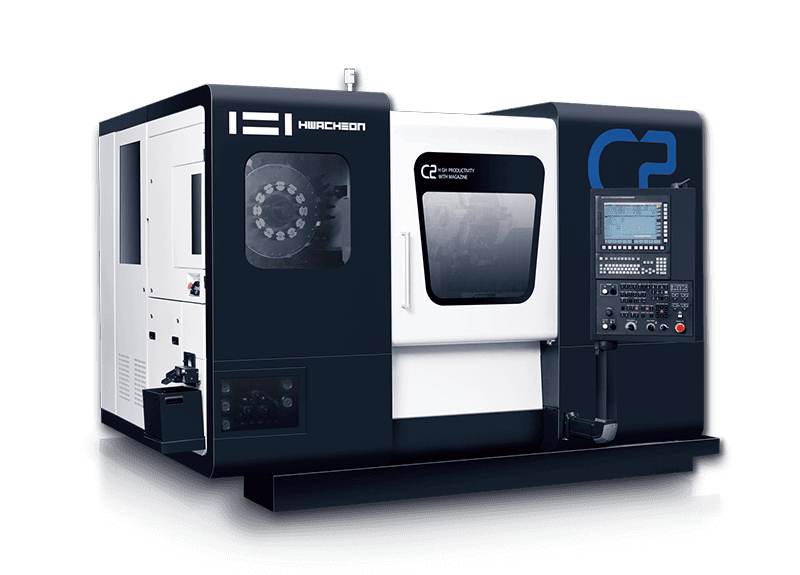
Hwacheon's C1 and C2 add a magazine: an 18-station Capto C4 turret works with a 12-tool magazine and an automatic tool changer. That is 29 tools in all, 18 on the turret and 11 in the magazine, which keeps one pocket empty for the exchange (catalog p. 10). Hwacheon describes them as turning centers with a machining center's capability through the Y and C axes (p. 3). They have no tilting head.
What does a B-axis milling head add?
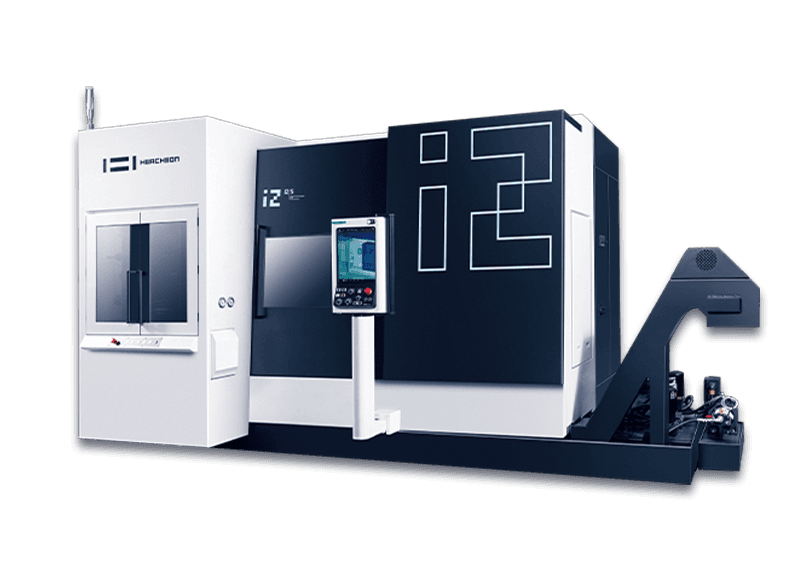
A milling spindle that tilts. On Hwacheon's i2, a 12,000 rpm HSK-T63 spindle (20,000 rpm and CAPTO C6 optional) swings ±120° on the B axis and indexes in 0.0001° steps, or in 5° steps clamped on a Curvic coupling (catalog p. 5). The program sets the angle. On a turret, the holder sets it: live holders point along the part or across it, and any other angle takes a holder set to that angle, such as the adjustable live spindle in Eurotech's Ultima brochure (p. 15).
A 40-tool magazine (80 optional) feeds the head and can be loaded while the machine cuts. Two 5,000 rpm spindles with 8 in chucks take Ø2.56 in (Ø65 mm) bar, the Y axis travels ±5.91 in (±150 mm), and the i2 cuts to Ø23.62 in (Ø600 mm) and 43.31 in (1,100 mm) long. Hwacheon designed it for complete machining of complex parts in a single setup (p. 3).
Programming is part of the choice. On the i2, Hwacheon's H-DRAW TC conversational programming, which covers B-axis work, and H-SIMUL iX interference checking are standard (p. 3, 10). Simultaneous 5-axis control is an option (p. 8).
The i2 sits in Hwacheon's multi-tasking turning centers with the C1, C2 and T2.
How do you tell which one your part needs?
- Where are the milled features? On the end face or the diameter: live tools. Off the centerline: a Y axis. On the back end: a sub-spindle. At one angle: a live holder set to it. At several angles: a B-axis head.
- How many tools does the whole part take, both ends? Compare it with the turret, then with a magazine.
- How big is the part, and does it start as bar? Size and bar capacity rule a machine in or out before any feature does; the model pages list both.
- How many setups does the part take today? A step earns its place when it takes one away.
Mostly milled, with little turning? That may be a machining center job: see 3-axis, 4-axis or 5-axis. More turrets is a different question: see twin-turret or single-turret lathe.
What should you send for a quote?
The part, the material and how many you make a year, plus the machines it runs on now: the quote form asks for each.
Common questions
What is a multitasking lathe?
A lathe that also mills, drills and taps, so a part comes off finished in one setup. The term covers a range: Hwacheon's multi-tasking turning centers do it with tool magazines, twin spindles and, on the i2, a B-axis milling head.
What is a B-axis turn-mill?
A turning center with a milling spindle that tilts on a B axis and a tool magazine to feed it. On Hwacheon's i2, the 12,000 rpm HSK-T63 spindle swings ±120°, the magazine holds 40 tools (80 optional), and two 5,000 rpm spindles hold the part, so turning, milling, drilling and tapping happen in one setup.
What does a sub-spindle add?
The back end, in the same setup. The sub-spindle takes the part from the main spindle and holds it while the second end is machined. With its own C axis, live tools work on that end too, as on Eurotech's single-turret machines, which pair a live turret and a Y axis with a sub-spindle with C axis.
Sources
- 1.Hwacheon i2 catalog: Precision Integrated Turn-Mill Center · hwacheon.com
- 2.Hwacheon C1 / C2 catalog: Horizontal Turning Center with Magazine & Y-Axis · hwacheon.com
- 3.Hwacheon Hi-TECH 350 catalog: Horizontal Turning Center, Box Way, Y-Axis · hwacheon.com
- 4.Hwacheon CUTEX-180 catalog: Chucker Horizontal Turning Center · hwacheon.com
- 5.Hwacheon T2 catalog: Integrated Multi Axis Turning Center · hwacheon.com
- 6.Eurotech Ultima Series B620 51 / 70 / 80 brochure · eurotechelite.com